BMR Machinery
Engineering Excellence
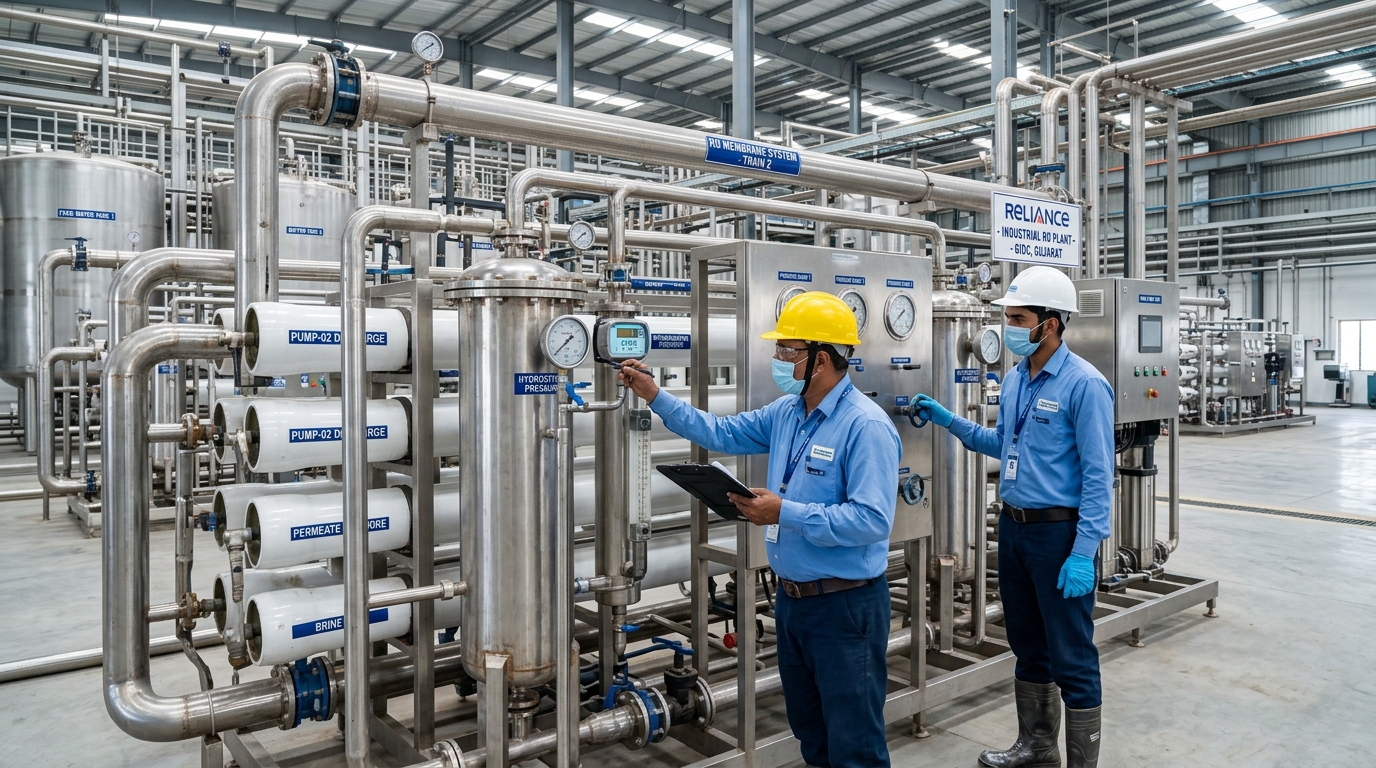
Discover the highly advanced Industrial RO Water Purification Plant by BMR Machinery. Engineered for maximum efficiency, speed, and durability. Get a quote today!
Water is the universal solvent, meaning it absorbs minerals, chemicals, and biological contaminants from everything it touches. For the bottled water industry, pharmaceutical manufacturing, and food processing, municipal or borewell water is entirely unusable in its raw state. The BMR Industrial RO (Reverse Osmosis) Water Purification Plant is a massive, multi-stage, high-technology filtration fortress designed to strip water down to its pure molecular state (H2O), removing 99.9% of dissolved solids, heavy metals, bacteria, and viruses.
We do not just build filters; we engineer complete water treatment ecosystems. A high-capacity RO plant must handle severe fluctuations in raw water quality, operate continuously without membrane fouling, and deliver water with an exact, specified TDS (Total Dissolved Solids) and pH level every single second. BMR Machinery utilizes aerospace-grade membranes, ultra-high-pressure stainless steel pumps, and intelligent PLC systems to create RO plants that are rugged, fully automated, and incredibly efficient.
Osmosis is a natural process where water moves across a semi-permeable membrane from an area of low salt concentration to high salt concentration. Reverse Osmosis forces the exact opposite. By applying immense pressure (often up to 300 PSI) using specialized multi-stage pumps, we force contaminated water through a microscopic membrane.
The pores in a BMR-supplied RO membrane are approximately 0.0001 microns in size. To put that in perspective, a human hair is 70 microns thick, and a virus is about 0.02 microns. The membrane acts as a molecular bouncer—only pure water molecules can squeeze through. All dissolved salts (sodium, calcium, arsenic, fluoride), bacteria, viruses, and heavy metals are blocked, concentrated into a "reject" stream, and flushed away safely.
Our Industrial RO plants are custom-built based on raw water analysis, but our standard high-capacity commercial models adhere to the following rigorous specifications.
| Parameter | Specification | Details |
|---|---|---|
| Output Capacity | 1,000 LPH to 100,000 LPH | Custom scalable modular skids |
| Raw Water Handling | Up to 3,000 ppm TDS | Brackish water and high-hardness capable |
| Purification Rate | 98% to 99.5% Rejection | Removes heavy metals, viruses, and salts |
| Membrane Type | Thin-Film Composite (TFC) Polyamide | Dow Filmtec / Hydranautics premium elements |
| High-Pressure Pump | Vertical Multi-Stage SS316 | Grundfos / CNP for vibration-free 300 PSI |
| Pre-Filtration | Sand, Carbon, & 5-Micron Micron | Protects RO membranes from physical fouling |
| Control Automation | Fully Automated PLC + Sensors | Auto-backwashing and auto-flushing standard |
| Piping Material | UPVC (Pre-RO) / SS316L (Post-RO) | Ensures zero leaching and absolute hygiene |
| Post-Treatment | Ozonation & UV Sterilization | Double-barrier protection against bacteria |
A true BMR Industrial RO Plant is never just a membrane. It is a highly strategic sequence of defensive barriers, designed to purify the water and protect the expensive RO membranes from damage.
The BMR RO Plant is highly adaptable and serves as the lifeblood for numerous sectors:
In the packaged drinking water business, the RO plant is your actual "product" manufacturer. Without it, you have nothing to sell. A high-quality BMR RO plant ensures you never suffer from "batch rejections" due to bad taste, smell, or bacterial contamination, which can destroy a brand's reputation overnight.
Furthermore, our systems are designed with high recovery rates. Cheaper RO plants often waste 60% of the raw water as reject. BMR plants utilize advanced membrane arrays and recirculation loops to recover up to 65-70% of the water, drastically lowering your raw water and electricity pumping costs. The ROI on a premium BMR plant is often realized through these water and energy savings alone.
RO membranes degrade if not cleaned. BMR plants feature fully automated PLC control. The system monitors the pressure differential across every filter. When the sand or carbon filters get dirty, the PLC automatically triggers a backwash cycle in the middle of the night, cleaning the filters without human intervention. When the plant shuts down, the PLC automatically flushes the RO membranes with pure water, preventing salt crystals from forming overnight. This intelligent automation extends the life of your expensive membranes by up to 2-3 years.
1. What is the difference between a commercial RO and an Industrial RO? Commercial ROs (like those in restaurants) use small, low-pressure membranes and plastic pumps. BMR Industrial ROs use massive 8-inch fiberglass membrane housings, high-pressure SS316 multi-stage pumps, and are designed to run 24 hours a day, processing thousands of liters per hour.
2. How much water is wasted during the RO process? There is no "waste"; there is a reject stream that carries away the concentrated toxins. Depending on the raw water TDS, a BMR Industrial RO plant typically recovers 60% to 70% as pure water, while 30% to 40% is rejected. The reject water can often be reused for gardening or floor cleaning.
3. Why does RO water sometimes taste bitter or flat? Pure H2O has no taste. When RO removes all the natural minerals, the water can taste flat or slightly bitter due to a drop in pH. This is why BMR includes an automated Mineral Dosing system to add healthy minerals (like calcium and magnesium) back in, giving the water a sweet, refreshing taste.
4. How often do I need to replace the expensive RO membranes? With proper maintenance, anti-scalant dosing, and regular automated flushing (which our PLC handles), premium membranes typically last between 2.5 to 4 years before needing replacement.
5. Can this plant treat seawater? Standard RO plants are designed for brackish or borewell water (up to 3000 TDS). Seawater (35,000+ TDS) requires a specialized SWRO (Seawater Reverse Osmosis) plant, which uses completely different ultra-high-pressure pumps (up to 1000 PSI) and specialized membranes, which BMR also manufactures.
6. Do we need an operator to run the plant all day? No. The BMR plant is fully automated. It connects to float sensors in your raw water and pure water tanks. When the pure water tank is full, the plant safely shuts down. When it drops, the plant turns on, flushes the membranes, and starts purifying automatically.
7. What is Ozonation and why is it necessary for bottled water? Ozone (O3) is a highly reactive gas. We inject it into the pure water just before bottling. It kills any bacteria that might have entered the bottles from the air. Crucially, Ozone breaks down into pure Oxygen after 24 hours, leaving no chemical residue, unlike chlorine.
8. Why do you use SS316 (Stainless Steel) piping after the RO membranes? RO water is highly "hungry" and slightly acidic because it has no minerals. If it runs through cheap iron or low-grade steel pipes, it will instantly corrode them and absorb the rust. We exclusively use food-grade SS316L stainless steel for all post-RO piping to guarantee absolute purity.
9. Can the plant remove heavy metals like Arsenic and Fluoride? Yes. The 0.0001-micron pores of the RO membrane are highly effective at rejecting heavy metals, pesticides, fluoride, arsenic, and lead, making it the most effective technology for handling severely contaminated borewell water.
10. What information do you need from me to build the RO plant? Before designing the plant, we require a comprehensive "Raw Water Test Report" from a certified laboratory. We need to know the exact TDS, Hardness, Silica content, Iron levels, and pH of your specific borewell water to engineer the correct pre-filtration and membrane configuration.
Calculate your potential earnings with BMR Machinery
Includes Preform, Cap, Label & Electricity
Daily Profit
₹80,000
Yearly Profit
₹2,49,60,000
Note: This is a rough estimation. High-speed BMR machines reduce per-bottle electricity cost by up to 20%, increasing actual profits further.
Speak directly with our engineers to configure the perfect Industrial RO Water Purification Plant for your production facility.
Chat on WhatsAppCall 091376 87609Email Sales TeamReliable, efficient, and built to last — their machines have transformed our production line. Output doubled in 3 months!
BMR Machinery delivered a fully integrated mineral water plant setup on time. We've seen a 30% increase in output since installation.
Exceptional performance and great after-sales service. They truly deliver what they promise. Highly recommended!